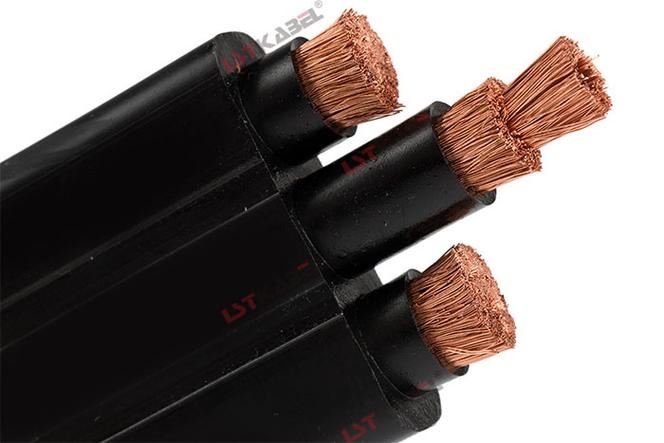
Detailed Description
Main Power Reel — The Single Most Critical Cable
A bucket wheel stacker reclaimer operates at 1 000–10 000+ tonnes per hour. Every minute of downtime represents 15–170 tonnes of lost production. The main power reel cable is the single point of electrical failure for the entire machine — if this cable fails, the machine stops.
The main power reel cable must:
- Deliver 1–3+ MW continuously at 3.6/6 kV or 6/10 kV through 100–500 m of cable on a motorized drum
- Survive 15+ winding layers on the drum — the innermost layer experiences sustained compression from all layers above it
- Handle the moving machine's full travel — winding and unwinding continuously as the machine traverses the stockyard
- Integrate control and fiber — the reel cable is the logical place to combine all machine connectivity in one cable pull
Deep Drum Engineering — What Happens at Layer 15
At 15 winding layers deep, the innermost cable experiences compressive force equal to the winding tension of all 14 layers above it — plus the cable's own weight. For a 400 m, 95 mm² MV cable at 12 kg/m with 60 kN winding tension:
- Cable weight on drum: 400 m × 12 kg/m = 4 800 kg ≈ 47 kN
- Compressive force at bottom layer: ~60 kN (outermost) + 47 kN (weight) ≈ 107 kN distributed across the drum surface
- Result: the inner cable layers are under sustained pressure equivalent to a 10+ tonne load
- Conductor deformation (copper cross-section flattening — increases resistance, creates hot spots)
- Insulation thinning (EPR permanent compression — reduces dielectric strength)
- Jacket cold-flow (PVC jacket permanently deforms and thins — CR and PUR resist this)
Travel Distance vs Drum Capacity — The Design Trade-off
| Travel Distance | Cable Length | Typical Cross-Section | Drum Layers | D/d Requirement | Tensile Rating |
|---|---|---|---|---|---|
| 100 m | 120 m (+20%) | 95 mm² | 4–6 layers | 15:1 | 30 kN |
| 200 m | 240 m | 120 mm² | 8–10 layers | 18:1 | 40 kN |
| 300 m | 360 m | 150 mm² | 10–12 layers | 18:1 | 55 kN |
| 400 m | 480 m | 185 mm² | 12–15 layers | 20:1 | 65 kN |
| 500 m | 600 m | 240 mm² or parallel | 15+ layers | 20:1 | 80 kN |
Above 400 m travel, the cable weight becomes the dominant design constraint. The drum must be large enough to accommodate the number of layers, the steel core must be strong enough to support the cable weight at full unwind, and the jacket must survive sustained compression at the drum bottom.
Control and Fiber Integration — Why NOT a Separate Cable
Some machine designs run a separate control/fiber cable on its own small reel. This adds:
- A second motorized reel mechanism to purchase, install, and maintain
- A second cable to synchronize with the main power reel during travel
- A second potential failure point
Why Choose Yichi Cable Reclaimer Reel?
- MV + deep-drum engineering combined: We understand the interaction between MV insulation requirements (semiconductive screens, PD testing) and deep-drum mechanical requirements (compression resistance, tensile reinforcement)
- 100% PD tested: Every meter of MV reel cable is partial discharge tested at 2 U₀ — a PD failure in the middle of a 400 m reel cable means scrapping the entire cable
- Compression-tested construction: Our core assembly is tested under simulated 15-layer compression — conductor roundness maintained within ±3% at rated load
- Control + fiber integration: In-house fiber cabling means the optical fibers are integrated during cable manufacturing — protected by the same quality process as the power conductors
- Stockyard travel calculation: Send us your machine travel distance, cable routing, and power requirement — we calculate the optimal drum diameter, cable cross-section, and tensile reinforcement